Pre-Shipment Inspection for Furniture Orders from China: How AQL Sampling Actually Works
The short answer: a pre-shipment inspection (PSI) is a check carried out on the finished, packed goods before they leave the factory, once production is 100% complete and at least 80% of the order is in export cartons. It uses AQL sampling under ISO 2859-1: you choose an inspection level, the lot size fixes your sample size, and the batch passes or fails on how many defects are found in that sample. A common starting point in furniture and general consumer-goods inspections is AQL 2.5 for major defects, 4.0 for minor defects, and zero tolerance for critical defects, but these values must be agreed in the purchase contract before production starts. ISO 2859-1 provides the sampling mechanics; it does not impose specific AQL values on a product category.
That is the mechanical answer. The commercial answer matters more: an inspection is a gate in your payment sequence, not a certificate. It tells you whether the sampled lot met the agreed acceptance criteria under the inspection plan, while your balance payment is still in your hands. It does not tell you the supplier will pass next order, it does not replace the documentation your destination market requires, and it does not mean zero defects. A buyer who understands what a pass buys, and what it does not, gets more value from the same inspection than a buyer who treats the word “passed” as an all-clear.
This article covers what a pre-shipment inspection is and is not, the four checkpoints a furniture order passes through, how AQL sampling works through a worked furniture example, a sample size table by lot size, how to classify critical, major and minor defects with real furniture examples, what a usable report contains, who should pay and how to keep the inspector independent, how the inspection gate ties to your payment release, what to do when an inspection fails, and what a pass genuinely guarantees.
What a pre-shipment inspection is (and what it is not)
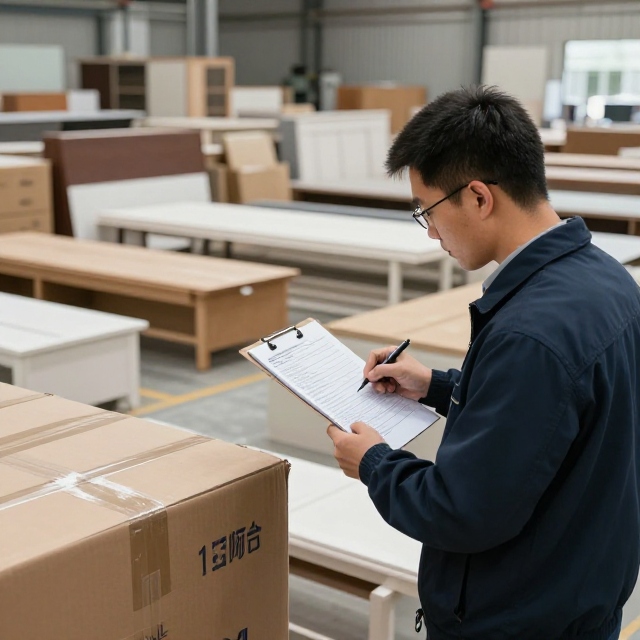
A pre-shipment inspection happens at one specific moment: production finished, most of the order packed, nothing shipped yet. The inspector opens cartons, pulls a random sample using the AQL rules below, and works through a written checklist: packaging, appearance, function, dimensions, quantity and labelling. The goods are still in the factory and your balance payment is still unpaid, which is the entire point of the timing.
Four things get confused with it, and each is a different service:
On that last point, this article is written from the buyer’s side. We coordinate sourcing and production from China for importers, and the guidance below is what a buyer should demand regardless of who performs the check.
The four checkpoints in a furniture order
“Inspection” is not one event. A full quality programme for a furniture order has four checkpoints, and the difference between them is when they happen and what failure costs at that moment.
| Checkpoint | When | What it catches | When it earns its cost |
|---|---|---|---|
| Pre-production (PPI) | Before mass production starts | Wrong or off-spec raw materials, packaging that does not match contract, tools and processes not ready | New factory, new product category, appearance-critical goods |
| During production (DUPRO) | When 10–30% of the run is complete | Systemic drift while there is still time to fix it mid-run: dimensions, workmanship, colour, assembly | Large orders, long production cycles, any risk of batch-wide error |
| Pre-shipment (PSI) | 100% complete, 80%+ packed | Finished, packed goods against specification, sample, packaging file and quantity | The default on every order |
| Loading supervision | Container loading day | Right quantities loaded, cartons undamaged, container clean and dry, seal recorded | LCL shipments, high-value goods, mixed-load risk |
Furniture has a specific reason to care about the early checkpoints, because its failure modes start in the raw material. A structured furniture programme checks timber moisture content as panels arrive, so wood has acclimatised to the destination market’s humidity range rather than splitting after a dry winter. It checks foam density and indentation load deflection against the spec sheet, because comfort is decided before the first seam is sewn. It checks fabric weight and composition against the written specification. Each of those is a fraction of the cost of discovering the same problem inside a finished, packed room.
The during-production checkpoint deserves a word of its own on furniture, because that is where the category’s expensive mistakes originate. Frames and joinery are checked against the construction drawing while the frame is still open: joints, dowels, screw lines and glue lines, because a structural failure found at pre-shipment sits inside a finished, upholstered unit that has to be dismantled to repair. Finishing is checked at the same visit: sanding quality, stain consistency, lacquer build and drying times, because a colour or sheen problem caught here can still be corrected across the run before the whole batch carries it. Hardware fit is checked while replacement parts are cheap to fit. The same visit verifies that the specified materials have actually arrived and are being used, which is the earliest moment a substitution can be caught, while it still costs a phone call rather than a container.
These checkpoints also sit at known points in the hotel furniture manufacturing process, which is why the schedule is easy to attach to milestones you already hold: raw material arrival, first-article and early production, finished and packed, loaded. The practical rule from inspectors who do this daily: for a first order with a new factory, pair a during-production check with the pre-shipment inspection. For a repeat order with a factory whose internal quality records you have verified across previous shipments, the pre-shipment inspection alone usually carries the decision. If you only ever book one stage, book the pre-shipment one.
How AQL sampling actually works
The standard behind it
AQL sampling is governed by ISO 2859-1, “Sampling procedures for inspection by attributes”. The current edition is ISO 2859-1:2026, the third edition, published in January 2026, which replaces the 1999 edition and its amendments, adds skip-lot sampling procedures and updated switching guidance, and is used alongside ISO 2859-0 for worked examples. The same tables appear as GB/T 2828.1 in China and as ANSI/ASQ Z1.4 in the United States, which is why two inspectors trained on different documents will pull the same sample from the same lot.
ISO’s own wording defines the acceptance quality limit as the maximum average percentage of defective items considered acceptable during random sampling, and states the standard’s purpose plainly: to put economic and psychological pressure on the producer to keep the process average at least as good as that limit, while bounding the risk to the buyer of accepting an occasional poor lot. Read that carefully, because AQL is not a statement that your lot contains a known percentage of defects, and it is not a promise about any individual unit. It is a property of the sampling plan: the acceptance and rejection numbers are calibrated so that a lot is judged on evidence drawn from it, with a defined risk of accepting a lot whose true defect rate is worse than the limit. The practical consequence is the same either way: without an agreed limit in the contract, the inspector has nothing to judge against.
Two parameters, then the table
Running an AQL inspection takes two decisions and one lookup.
Deciding the lot, and deciding the threshold
Before any table lookup, one question decides everything: what counts as a single lot? For furniture the honest answer is usually per purchase order line, split further when the line mixes SKUs, colours or sizes with different risks. A container holding sofas, tables and cabinets is three lots in practice, because each product has its own failure modes and its own packaging construction, and a sample drawn across a blended pile tells you very little about any one of them. Define the lot in the order confirmation, the same way you define the thresholds, so that “the inspection” refers to a decision about specific goods rather than an argument about which cartons were in scope.
Choosing the threshold is a risk decision with three inputs: how visible the surface is to the guest, how much assembly and function the product carries, and what the consequence is if it fails in use. Aesthetic, high-touch items with complex assembly justify a tighter major threshold than a value-positioned programme where the buyer has consciously accepted a looser minor rate in exchange for unit pricing. Safety-related content pushes the classification to zero regardless of the commercial trade-off. What matters is that the reasoning is written down before production, because the same threshold is impossible to negotiate honestly after a report has failed it.
A worked furniture example
An order covers 5,000 nightstands on one purchase order line. Under General Inspection Level II, single normal sampling, a lot of 3,201–10,000 units gives a sample of 200 units. At major AQL 2.5, the acceptance number is 10 and the rejection number is 11: find 10 or fewer major defects in the sample and the lot passes that class; find 11 and it fails. At minor AQL 4.0, the same sample accepts up to 14 and rejects at 15.
Three rules do most of the work in practice. Majors and minors are counted separately, never combined, because they carry different thresholds. Where the contract specifies zero acceptance for critical defects, a single critical defect fails the lot, so there is no counting to do. And once a class reaches its rejection number, the lot can be rejected under the agreed sampling plan; the inspector does not need to complete the remaining sample for that class, which saves time and gives the factory nothing to argue with.
The standard itself is not free, so the tables below are the Level II single-normal-sampling figures as published in the inspection-industry guides cited in this article, which reproduce the ISO 2859-1 and ANSI/ASQ Z1.4 tables. If your programme runs a different level or a double-sampling plan, your inspector’s report should state which plan it used.
Sample sizes by lot size
| Lot size (units) | Sample size (General Inspection Level II, Single Normal Sampling) | Major AQL 2.5: accept / reject | Minor AQL 4.0: accept / reject |
|---|---|---|---|
| 91 – 150 | 20 | 1 / 2 | 2 / 3 |
| 151 – 280 | 32 | 2 / 3 | 3 / 4 |
| 281 – 500 | 50 | 3 / 4 | 5 / 6 |
| 501 – 1,200 | 80 | 5 / 6 | 7 / 8 |
| 1,201 – 3,200 | 125 | 7 / 8 | 10 / 11 |
| 3,201 – 10,000 | 200 | 10 / 11 | 14 / 15 |
| 10,001 – 35,000 | 315 | 14 / 15 | 21 / 22 |
Read it as a contract, not as advice. A run of 1,200 units means 80 inspected, five majors accepted, six rejected. Notice what the table does not do: it does not scale with how good you want the goods to be. That is the second decision, the AQL value, and it is yours to set before production rather than the inspector’s default on inspection day.
Two more mechanics from the standard are worth knowing because they show up in real reports. The standard carries switching rules: inspection starts normal, tightens when lots start failing, and relaxes to reduced inspection when a supplier’s record is consistently good, with skip-lot procedures added in the 2026 edition. In practice this means a supplier with a clean history earns less sampling, and one with two failed lots earns tighter scrutiny. It also means the inspection history you keep across orders has direct commercial value: the record is what justifies either direction.
Critical, major and minor: classified with real furniture defects
The classes are defined by consequence, not by appearance. A critical defect makes the unit unsafe or unsaleable, and any occurrence fails the lot. A major defect is one a buyer would reject if they examined that unit individually: it affects function, fit or the customer-facing finish. A minor defect is something a buyer would normally accept but which signals drifting discipline. Where a defect sits matters as much as what it is: the same scratch on a desk top is a major defect and on the underside of the same desk top is minor.
| Class | Furniture examples | Threshold practice |
|---|---|---|
| Critical | Unstable structure or sharp unsafe edge, a load-bearing joint that fails, a missing warning or anti-tip instruction where the destination requires one, severe contamination | Zero: any occurrence fails the lot |
| Major | Wrong dimension against drawing, visible finish defect on a customer-facing surface, edge banding lifting on a desk top, seam pucker on an upholstered front, colour banding across the run, drawer glide that does not operate, missing hardware, failed assembly of a knock-down unit | Common starting point: AQL 2.5 |
| Minor | Small hidden rub, slight underside scuff, minor carton blemish, negligible glue mark on a non-visible face | Common starting point: AQL 4.0 |
Two points make the classification actually usable. First, severity follows the specification you wrote: a finish defect on a visible face is major because the written spec made that face customer-facing, and the identical mark on a carcass interior is minor. This is where the surface decisions from the HPL, melamine and veneer comparison feed directly into inspection: the defect list the inspector works from should name which surfaces are graded strictly and which are not, agreed before the inspector arrives. Second, a missing screw is not automatically major or minor: if its absence makes the unit unsafe, it is critical. Defect classification has to be decided by use and consequence, not by a generic list copied from another product.
When safety rules make classification non-negotiable
Destination-market law can override any grading discussion. For the United States, clothing storage units (free-standing furniture with drawers or hinged doors for storing clothing, at least 27 inches tall, at least 30 pounds, with at least 3.2 cubic feet of enclosed storage) are regulated under 16 CFR part 1261 for units manufactured after 1 September 2023. The rule incorporates ASTM F2057-23, requires stability testing under specified loading and force conditions, requires an anti-tip device meeting ASTM F3096 to be packaged with the product, and requires warning labels with specified statements. Certification paperwork for such units cites 16 CFR part 1261.
So on a US-market order that includes such a unit, a missing anti-tip device in the carton or a missing warning label is not a minor packaging finding. It is a critical defect with a regulatory citation behind it, and it belongs in your defect classification before the inspection, not in the argument after it. The equivalent exercise for any other destination is short: name the rules that apply to your product category and market, and put any gap in them into the critical column.
What the report should contain, and how to read a conditional pass
A usable inspection report is a short document with specific fields. If any of these are missing, the report is closer to a marketing document than a control:
Quantity deserves its own line because it is the finding with no second chance. A short shipment is one of the most common cross-border disputes, and it is provable only while the goods are still countable in the factory against the packing list. The count is done carton by carton with units per carton verified, and mixed orders are checked ratio by ratio (a colour mix that is right in total but wrong per colour is still a wrong shipment). The same discipline applies to labelling: shipping marks, carton contents, barcodes that scan, country-of-origin marking, warnings in the destination language. One wrong character on a label or a mark that does not match the packing list can hold a shipment at destination customs long after the quality question has been settled.
Function and assembly checks are where furniture inspection either earns its fee or becomes a tick-box. For knock-down furniture the sampled units are assembled, or at least the critical fit points are verified: hardware holes, cam locks, dowels, brackets, hinges, rails and threaded inserts all align, the hardware bag contains what the instruction sheet says it should, and the instructions themselves produce a unit that goes together. Stability checks are defined in advance by the buyer: wobble, drawer glide, door gap, leg attachment, table level, shelf fit. The buyer defines simple, reasonable checks; the inspector should not invent unsafe stress tests on the factory floor, and any formal safety testing belongs in the lab or the compliance programme where the destination market requires it. Moisture and odour findings matter on wood, panels and upholstery bound for a long ocean shipment, and damp cartons or a chemical smell photographed at the factory are far cheaper to act on than at the destination warehouse.
The brief the inspector works from decides how much the report is worth. That brief should be built from your written specification and exclusions, with tolerances, a photo set showing acceptable versus unacceptable for each likely defect, your critical and major and minor classifications, function tests with pass criteria, and a reference to the approved golden sample rather than a glossy prototype. A generic instruction to “check the goods” produces a generic report, and a generic report cannot settle a dispute. The scope discipline that keeps the inspector’s checklist enforceable is the same discipline that keeps the package priced correctly: hotel FF&E scope and exclusions.
Results come in three practical forms. Pass: the sampled goods met the agreed inspection thresholds and, subject to the other contractual and regulatory requirements, the lot is cleared for shipment. Pass with condition: minor issues with no impact on use; either the factory corrects and you verify, or you accept the specific issue list in writing as a waiver, because an unrecorded conditional pass is worth nothing later. Fail: thresholds exceeded; rework, then re-inspection. Read past the verdict page either way: a pass with a cluster of major defects sitting just under the rejection number is information about the next batch, and about whether your threshold is set where it should be.
Who pays, who appoints, and how to keep it independent
This is the question most comparison pages avoid, because most of them sell inspections. The buyer arranges and pays for the inspection. The reason is structural: the inspector’s independence rests on reporting to the party appointing and paying them, and an inspection arranged and controlled entirely by the supplier provides less independent evidence than one appointed and received directly by the buyer. Factories sometimes offer to cover the cost as a gesture. Declining it is the cheaper decision.
On cost, the figure moves with the number of SKUs and cartons to check, the required scope, how many man-days the order needs and where the factory is, so compare quotations on the same written scope rather than on a headline day rate, and price re-inspections at roughly the same cost again when you budget. Either way, treat inspection as a fixed line in landed cost rather than an optional extra.
Three scheduling facts matter more than the price. Book the inspection for 7 to 10 days before the planned container loading date, which gives the factory time to address findings without destroying the freight booking and gives you time to review the report before the balance is due. Give the inspection company several working days’ notice, more in peak season. And make the visit unannounced to the factory’s own quality team where possible: the factory will know an inspection is coming, but it should not be able to hand-pick which day the sample pile looks best.
The sample pile is the second independence point, after who pays. Random selection only works if the inspector draws the sample from the whole lot, and a factory that has stacked the easy cartons at the front, or that offers to assemble the sample for the inspector, has quietly converted a random sample into a curated one. Let the inspector open cartons, choose units across the lot and record which cartons and units were sampled. The same applies to the report itself: it should be addressed to you and sent to you, with its photographs and raw counts, without a factory translation or summary attached in between. Independence is not a badge on the letterhead; it is who selected the sample, who receives the evidence, and who pays the invoice.
Who chooses the firm: you do, and no particular name is required. What to verify instead of a brand: independence from the factory, experience in your product category, a report structured against AQL with the fields listed above, and a sample distribution covering your SKUs. Where your own customer or a regulated channel mandates a particular agency, that constraint decides it for you. Where a buyer is on site, a buyer’s own attendance at a hero SKU or a launch batch is a legitimate model, at the cost of travel and time.
Write the re-inspection money rules into the order confirmation before ordering: rework and re-inspection caused by factory quality problems fall on the factory, re-inspection caused by your changed requirements falls on you, and the maximum number of re-inspection rounds before the order is restructured is stated. Negotiating any of that on the day a report comes back means negotiating against a party with the goods.
Tying inspection acceptance to your payment release
The inspection only has leverage if it sits before the money moves, and there is a subtle version of this that buyers get wrong. On a typical first programme the structure is a deposit at order confirmation and a balance against the pre-shipment inspection. The subtlety: the trigger for releasing the balance should be your acceptance of the report, not the inspection event itself. If the inspection happens and you pay before you have read and accepted the findings, you have spent the leverage you were paying for.
The same logic runs one step further: do not let the freight booking precede report acceptance. A container booked against a planned ship-out date, with the inspection failing days before loading, produces exactly the pressure the sequence was supposed to prevent. Book freight against a confirmed pass, with a few days of float in the schedule.
The pressure looks like a phone call: the vessel is cut off, release the balance now and the factory will fix it on the next order. That promise is unenforceable once the goods are at sea and the money is gone, and every experienced buyer has heard it. The report is objective evidence a factory finds hard to argue with; it loses that value the moment the container leaves and the balance is released.
What to do with a failed inspection
A failure is a normal outcome, not a crisis, provided you work it in order:
Two cautions. Rework is itself a new production run in miniature: reworked goods must be re-inspected, never accepted on a phone assurance that everything has been fixed. And pressuring a buyer to accept a partial fix in exchange for a promise on the next order is the standard move, because the factory knows the evidence has an expiry date. Insist on sorting or repairing against a re-inspection while the goods are still in the factory, where a hammer and a set of replacement panels cost almost nothing.
What a “pass” does not mean
The honest caveat that inspection firms avoid selling is this: sampling carries an inherent miss probability. AQL sampling guarantees a statistically acceptable defect rate across a lot, not zero defects in every unit, which is why programmes with genuine zero tolerance use 100% inspection instead. A pass also does not mean the supplier is permanently reliable, because quality can drift on the very next order when a factory changes a material supplier, reorganises the line, or is simply rushed. One passed report certifies one lot on one day.
And a pass does not clear the shipment for entry. Customs and product-conformity documentation are a parallel track entirely: the certificates, declarations and shipment documents your destination market requires are assessed on the paperwork, and a clean quality report does not substitute for any of them. Where the route involves certification platforms and conformity certificates, that process has its own sequence and its own timing, as set out in SASO and GCC conformity for furniture imported from China. Inspection confirms the goods match your order; documentation gets the goods across a border.
What a pass does buy, and it is worth the money: objective evidence, dated and photographed, that this lot matched your agreed specification at the moment it left the factory, issued while you still held the balance, accepted before the freight was booked, and filed as part of a quality record. Over a few orders that record is the real product. It tells you whether a supplier is improving or slipping, and it is the evidence you hold when the next negotiation starts.
Questions buyers ask next
How far in advance should I book an inspection?
Seven to ten days before the planned container loading date is the workable window, with several working days’ notice to the inspection company and more during peak season. The window has to contain three things in order: the inspection itself, your review and acceptance of the report, and the rework plus re-inspection in case the first result is a fail.
How long does one inspection take?
One inspector for one working day, around eight hours, is typical for a standard order: pulling and checking a 200-unit sample takes roughly two to four hours and the remainder goes to the report. Larger lots, multiple man-days, 100% inspection and loading supervision are billed separately.
Who sets the AQL values?
You do, and they go in the purchase contract or order confirmation before production starts. Factories may propose different thresholds, so the buyer should agree the values with them before production rather than at inspection day. If you have no basis to choose, the common starting combination for furniture is major 2.5, minor 4.0, critical zero, as a starting point you have agreed rather than a standard imposed afterwards.
Is the factory’s own inspection enough?
Not for a first order, and not as the gate in front of your balance payment, because the party being checked is measuring itself on delivery and cost. Once a factory’s internal quality system has been verified across previous shipments, its documented self-checks can support a lighter cadence on repeat orders, but the independent check on the lot you are about to pay for is the one that protects the payment.
Can I inspect the goods myself?
You can, and buyer-on-site inspection is a legitimate model for hero products or launch batches. What a trained third party adds is consistent application of the AQL method and a report the factory cannot easily dispute. If you cannot attend, an independent inspector working to your written brief is considerably more reliable than the factory’s own quality department on the lot you are paying for.
Does a pass mean the shipment meets destination regulations?
No. A pass confirms the batch matches your specification, sample, packaging file and quantity. Regulatory entry depends on the documents and certifications your destination market requires, which are assessed separately on the paperwork. Where the scope includes safety-driven product rules for a destination market (for example the anti-tip requirements for clothing storage units sold in the United States), those belong in your pre-production documents and your defect classification, not in the assumption that a quality report covers them.
Does the inspection cover packaging for the journey?
Partly, and it is worth insisting on that part. Packaging checks inside a pre-shipment inspection cover carton strength and size, edge and corner protection, foam and divider placement, hardware bags secured so they cannot rub a finished surface, separation between metal parts and upholstery or veneer, moisture protection, instruction sheets, shipping marks and barcodes, and photographs of the internal protection rather than only the outside of the carton. What a standard inspection does not automatically cover is validated transit performance: drop testing, carton compression and transit simulation are separate packaging validations, worth specifying when the route, the stacking or the destination handling makes transport damage a real probability.
Should every shipment be inspected?
For a first programme with a new factory, yes, on every shipment, with a during-production check alongside when the order is large. As a supplier’s record builds, the rational cadence becomes risk-based: full inspection on the first batch of each new season, whenever a new SKU is introduced, whenever the destination market or compliance requirements change, and lighter treatment in between for stable repeat orders with documented internal quality records.
What is the difference between a factory audit and a product inspection?
An audit examines the supplier (licences, production lines, capacity, quality systems, whether it can deliver to spec over time) and is done rarely, typically once per supplier and then periodically. An inspection examines the goods of a specific lot and happens on every order. The audit helps you choose the supplier; the inspection decides whether this batch ships.
The sequence is the whole discipline: specification and defect classes agreed before production, the inspection scheduled against the loading date, the report read and accepted, the balance paid only after that acceptance, and freight booked only on a confirmed pass, with every report filed. Run in that order, an inspection is the cheapest control in the entire sourcing process. Run out of order, it is a receipt for a visit that changed nothing.